Call Us
+86-15800763021
Send Us
Add
775 Chihua Road, Zhelin Town, Fengxian District, Shanghai
- All
- Product Name
- Product Keyword
- Product Model
- Product Summary
- Product Description
- Multi Field Search
Views: 0 Author: Site Editor Publish Time: 2026-11-21 Origin: Site

The visual appeal of pomegranate juice is undeniable. Its vibrant, ruby-red hue signals freshness and a high antioxidant content to health-conscious consumers. Shoppers instinctively associate a deep, clear red with premium flavor and nutritional integrity. Maintaining this vibrant profile, however, is a notorious challenge on the factory floor. Without strict operational control, the liquid rapidly morphs into a muddy brown or dull brick-red. This degradation leads to widespread product rejection and significant financial losses.
The fruit itself is rarely the problem. An improperly configured processing environment is usually the primary culprit. The journey from raw aril to bottled beverage involves severe mechanical and thermal stress. Fluid dynamics, shear forces, and thermal loads all play a role in pigment destruction. Plant managers can successfully preserve the natural appeal of the product by understanding the underlying science of pigment loss and utilizing the correct hardware. This guide breaks down the chemical triggers of discoloration and offers actionable, machinery-based solutions to optimize your facility operations.
Preventing visual degradation in beverage manufacturing requires a solid understanding of the raw material chemistry. The vibrant appearance of the juice is not a static characteristic. It is a delicate biochemical balance requiring careful management throughout the entire production cycle.
A class of water-soluble pigments known as anthocyanins produces the distinct red, purple, and blue hues found in many fruits. Located deep within the vacuoles of the pomegranate arils, the primary anthocyanins include cyanidin, delphinidin, and pelargonidin glycosides. These pigments provide stunning visual appeal while acting as potent polyphenols directly tied to health benefits. Nutritional science indicates that these compounds act as strong antioxidants that neutralize free radicals. Preserving these compounds is therefore a matter of both aesthetic quality and nutritional integrity.
Anthocyanins are highly beneficial but notoriously unstable outside their natural cellular environment. The moment a pomegranate aril ruptures in the extraction machinery, these pigments are exposed to external factors that trigger rapid degradation. They react aggressively to ultraviolet light exposure, temperature spikes, and sudden shifts in pH levels. If the processing atmosphere is not strictly controlled in a standard industrial setting, the anthocyanin molecules undergo structural transformations. They shift from a stable red state to a colorless form and eventually break down into unappealing brown compounds.
Discoloration rarely happens due to a single catastrophic equipment failure. It is often the cumulative result of mechanical and chemical stressors throughout the facility. Identifying the exact stage where degradation begins is vital for optimizing pump speeds, holding times, and overall operations.
The most prevalent cause of pigment loss is enzymatic browning driven by oxidation. When pomegranates are aggressively crushed, the cellular structure of the arils is destroyed. This action releases Polyphenol Oxidase and peroxidase enzymes. A rapid catalytic reaction occurs once these enzymes mix with the anthocyanins and are simultaneously exposed to ambient oxygen. The enzymes oxidize the phenolic compounds into quinones, which then polymerize to form dark, melanin-like pigments. This biological process is identical to a sliced apple turning brown on a kitchen counter.
Heat acts as the second most significant threat to pigment stability. Thermal degradation occurs when the juice is subjected to excessive temperatures. This can happen unintentionally through mechanical friction during milling or intentionally during pasteurization. Sustained high temperatures literally cook the delicate anthocyanin molecules and break their glycosidic bonds. This thermal stress causes irreversible damage. Furthermore, excessive heat accelerates the Maillard reaction. This non-enzymatic browning process between amino acids and reducing sugars further darkens the product and introduces burnt off-flavors.
A less common but equally destructive cause involves chemical reactions between the juice and the processing equipment itself. Pomegranate juice is inherently acidic. If the liquid comes into contact with non-food-grade metals or older pipes constructed from carbon steel, the natural acids will leach transition metal ions like iron or copper into the flow. These metal ions react instantly with the anthocyanins to form stable, dark-colored metallo-anthocyanin complexes. This reaction turns the juice a dull, grayish-blue or muddy brown.
The extraction stage is the critical juncture where the raw fruit transforms into liquid. The mechanical method chosen here dictates the initial quality of the juice and sets the baseline for how well the hue will survive downstream processing.
Traditional high-speed extraction methods prioritize maximum yield over delicate handling. Centrifugal juicers and aggressive screw presses operate at high revolutions per minute. This generates immense mechanical friction and shear stress. The friction translates directly into heat, immediately raising the temperature of the raw juice. In addition, the aggressive tearing actions whip a massive amount of ambient air into the liquid matrix. The juice has already suffered severe thermal and oxidative damage by the time it exits a traditional high-speed press.
Industry leaders are increasingly adopting gentle pressing technology to combat the flaws of legacy systems. A modern Cold Press operates using hydraulic pressure to slowly squeeze the juice from the arils without high-speed rotary blades. The pressing action is strictly controlled, generating virtually zero friction and preventing temperature spikes. This method keeps the cellular structure intact for a longer period and drastically reduces the amount of oxygen forced into the liquid. It preserves the fresh, tart flavor profile that premium consumers expect.
| Processing Parameter | Traditional High-Speed Extractor | Modern Hydraulic Cold Press |
|---|---|---|
| Mechanical Friction & Shear | Extremely High | Near Zero |
| Oxygen Aeration | Severe mixing of ambient air | Minimal surface exposure |
| Temperature Rise | Increases by 5 to 10 degrees Celsius | Maintains ambient temperature |
| Initial Juice Quality | Cloudy, highly prone to rapid browning | Clear, stable ruby-red profile |
Raw pomegranate juice is cloudy directly following extraction. It contains suspended pulp, seed fragments, and insoluble fibers. The premium market segment generally demands a brilliantly clear product, necessitating a highly efficient clarification stage.
Clarification is the mechanical process of removing suspended solids from the raw liquid. These solids will eventually settle at the bottom of the bottle if left in the juice. More importantly, the suspended pulp contains high concentrations of active enzymes. These solids will continue to drive enzymatic browning if not removed quickly, degrading the visual profile long after the juice has been extracted.
Specialized separation hardware offers the most efficient industrial method for clarification. A high-quality Decanter centrifuge is engineered to handle high volumes of liquid containing heavy solid loads. It utilizes extreme centrifugal force, often exceeding 3000 revolutions per minute, to rapidly separate the heavier solids from the lighter liquid phase. A sanitary centrifuge operates as a hermetically sealed, closed-loop system constructed from SUS304 or 316L stainless steel. This ensures the separation occurs without exposing the juice to the ambient atmosphere, preventing the highly agitated liquid from oxidizing before it reaches the pasteurizer.
Mechanical upgrades are essential, but biochemical interventions in the formulation stage provide a necessary secondary line of defense. This intervention typically occurs in the mixing or holding tanks immediately following extraction and clarification.
Certain vitamins are utilized in industrial beverage processing for highly effective and safe antioxidation, rather than just nutritional fortification. Ascorbic Acid is a water-soluble compound that readily dissolves in fruit juices. It provides a protective barrier without negatively impacting the viscosity or mouthfeel of the final product.
The application of this antioxidant relies on the principles of redox chemistry. It neutralizes the dissolved oxygen present in the liquid when dosed correctly early in the production flow. It acts as a sacrificial shield. The oxygen molecules bind with the additive first because it is more reactive to oxygen than the anthocyanin pigments. This chemical reaction effectively starves the browning enzymes of the catalyst they require. It shields the delicate anthocyanins and preserves the ruby-red appearance.
Heat treatment is a non-negotiable step mandated by global food safety authorities to eliminate pathogenic microorganisms. However, it presents a significant engineering challenge regarding pigment preservation.
The dilemma lies in the fundamental relationship between temperature and pigment stability. The sustained heat required to achieve commercial sterility is exactly what destroys the anthocyanins. Traditional batch pasteurization holds the juice at moderate temperatures for extended periods. This inflicts massive thermal stress on the product and results in a dull, brownish liquid.
Modern facilities utilize High-Temperature Short-Time pasteurization to balance strict food safety requirements with optimal quality. This advanced thermal processing method utilizes highly efficient plate or tubular heat exchangers. The juice is rapidly heated to a much higher temperature, typically between 85 and 95 degrees Celsius, but is held there for only 15 to 30 seconds. The liquid is aggressively cooled back down immediately following this brief holding time. This rapid heating and cooling cycle achieves the required pathogen reduction while minimizing the total thermal load applied to the anthocyanins.
The product remains highly vulnerable during the final stage of manufacturing, even if a facility successfully navigates extraction, clarification, and pasteurization perfectly. Degradation can easily occur post-processing if the packaging stage is flawed.
The primary threat during this final phase is headspace oxygen. This is the volume of ambient air trapped between the surface of the liquid and the cap. The juice will slowly oxidize over time if standard atmospheric air is sealed inside the container. This trapped oxygen will cause the liquid to turn brown while sitting on the supermarket shelf, ultimately destroying brand trust, regardless of how perfect the product looked leaving the factory.
Manufacturers must invest in specialized Filling machinery to guarantee long-term shelf stability. Vacuum sealing systems mechanically extract the air from the bottle immediately before applying the closure. Alternatively, nitrogen dosing injects a blast of inert nitrogen gas into the headspace just before sealing to displace the oxygen. Aseptic environments provide the highest level of protection by performing the entire process inside a completely sterile, oxygen-free chamber.
Recent market analyses reveal a significant shift in the beverage manufacturing sector. The demand for clean-label, minimally processed juices has surged globally as consumers increasingly scrutinize labels for artificial dyes and synthetic preservatives. Top-tier producers are abandoning legacy thermal extraction methods in favor of non-thermal or highly controlled, gentle processing technologies.
This industry pivot is largely driven by the absolute necessity to maintain natural pigment integrity. This is specifically true for high-value, antioxidant-rich products like pomegranate and tart cherry juices. Facilities that fail to modernize their extraction and preservation methods find it increasingly difficult to compete on retail shelves. Superior Colour Retention often dictates the purchasing decision of the modern consumer. Investing in advanced fluid handling systems is no longer just about yield; it is about protecting the visual brand identity.
Diagnosing the root cause of degradation is only the first step for plant managers and beverage entrepreneurs. The ultimate solution requires a comprehensive audit of existing machinery and strategic capital investments to modernize the facility based on strict engineering standards.
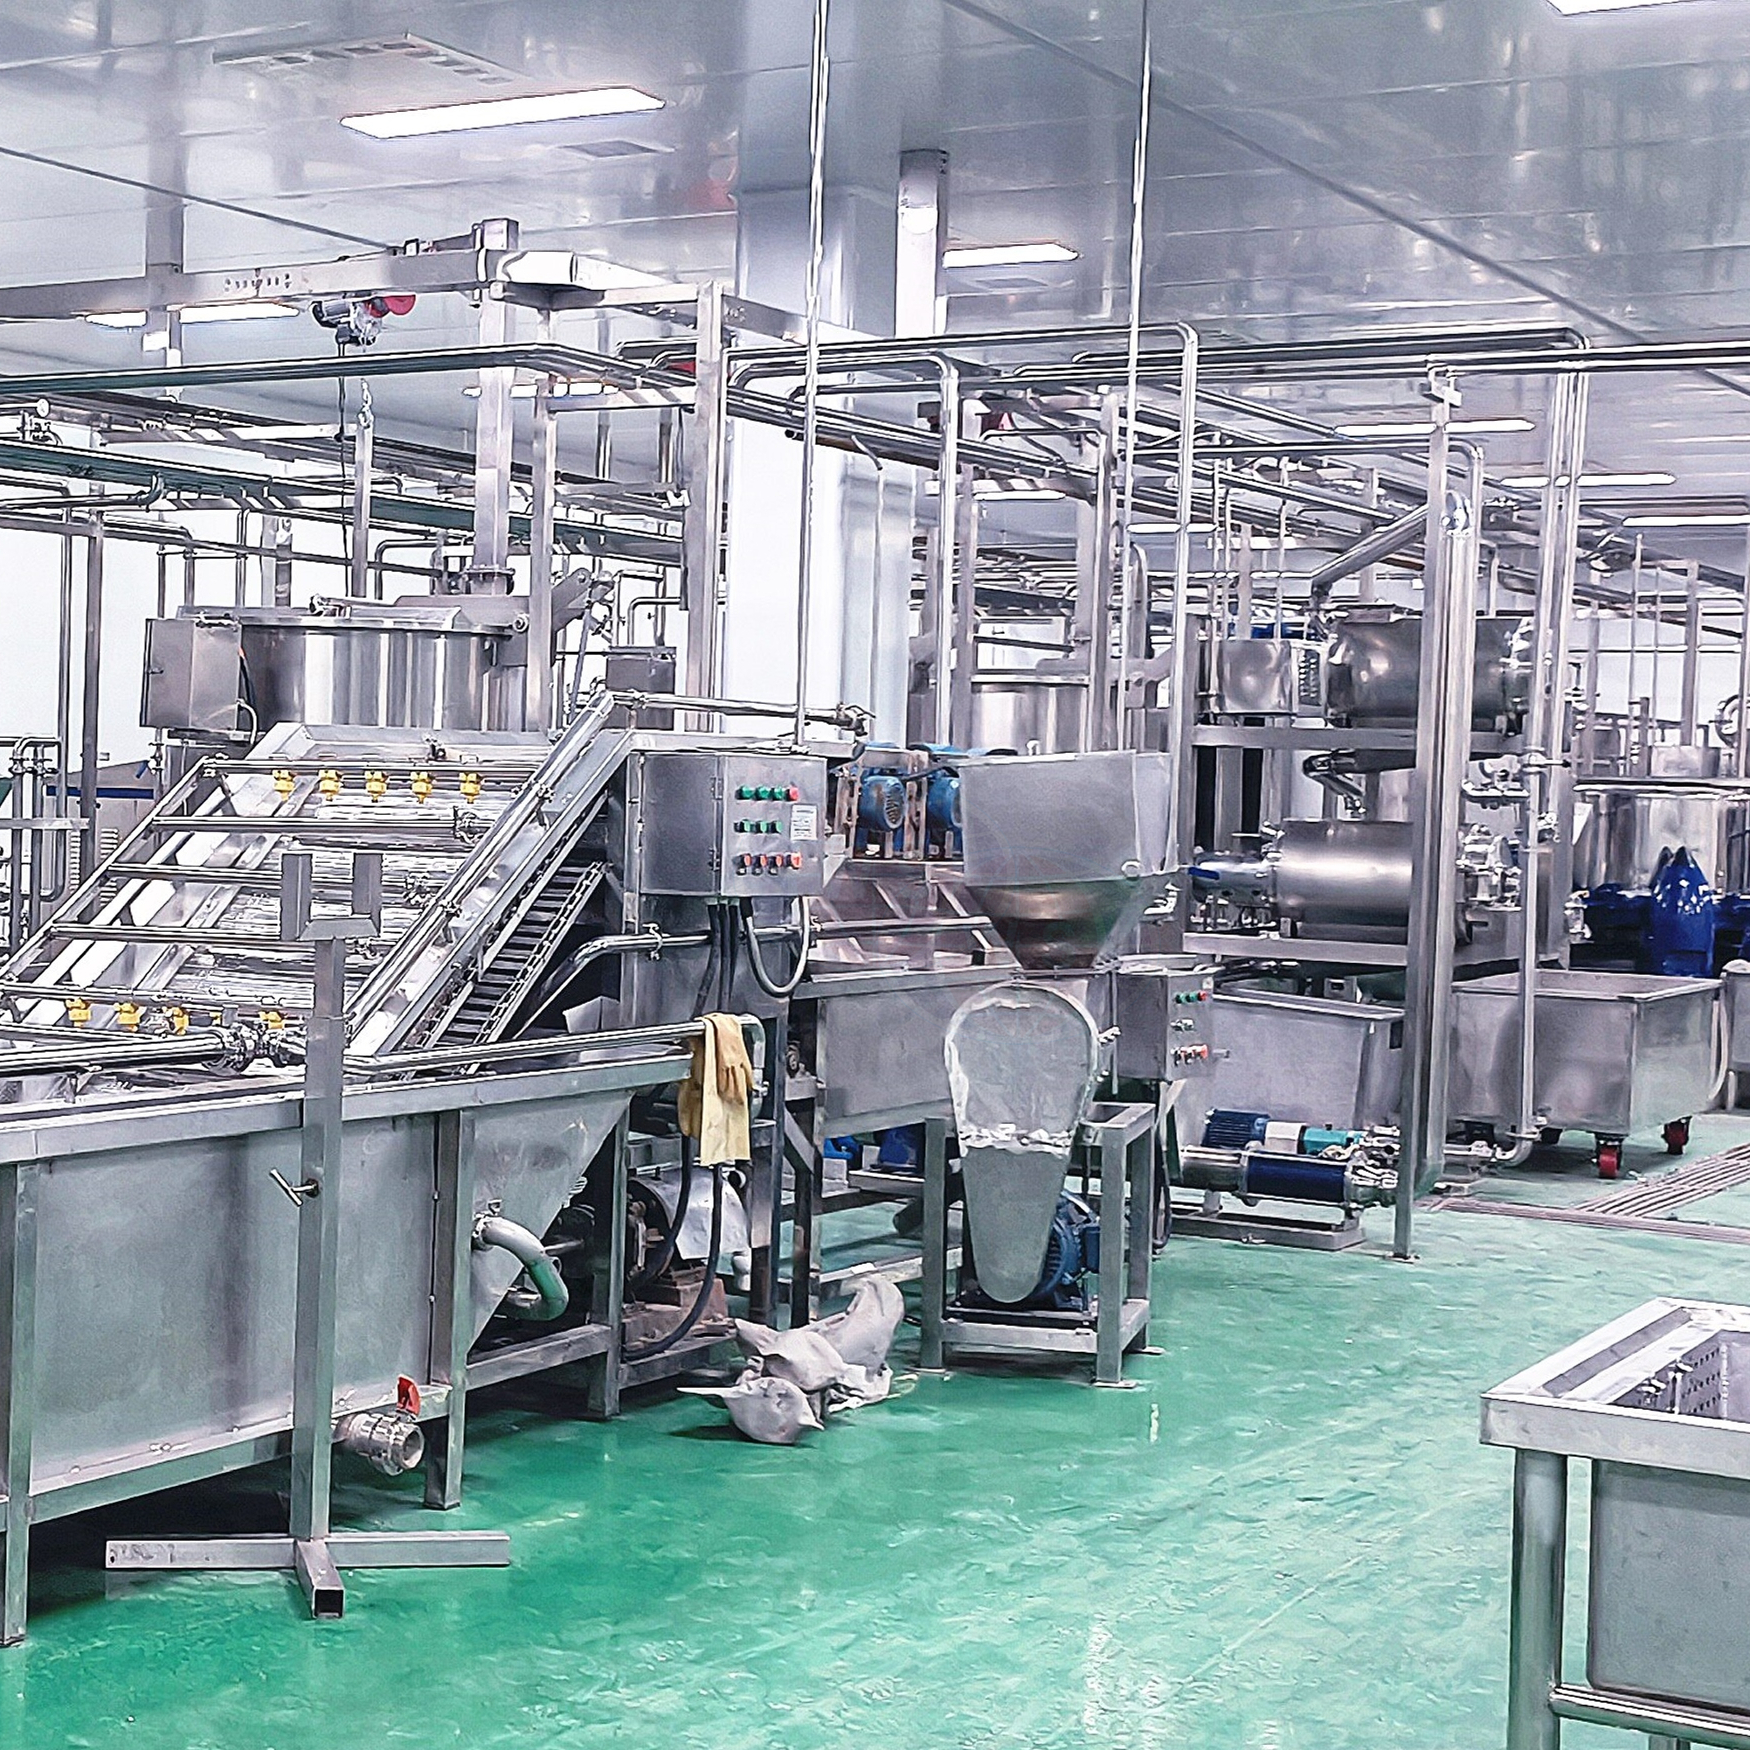
Transitioning to a fully enclosed production ecosystem is the most critical upgrade. The liquid should ideally never be exposed to the open atmosphere from the moment the fruit is pressed to the moment the bottle is sealed. Utilizing hermetically sealed tanks, enclosed transfer pumps, and in-line deaerators minimizes oxygen pickup drastically. Automated Clean-in-Place systems should be integrated to maintain absolute sanitation without dismantling the line.
The physical construction materials of the hardware must be rigorously evaluated. Every surface that comes into contact with the acidic juice must be constructed from high-grade sanitary stainless steel, specifically SUS304 or 316L. These alloys offer superior corrosion resistance. They ensure that no transition metal ions leach into the product to trigger chemical browning.
Off-the-shelf equipment designed for apples or citrus fruits is rarely optimal for pomegranates. The unique pH, high astringency, and specific viscosity require tailored engineering. Buyers should seek out manufacturers capable of customizing the entire line for specific capacities, typically ranging from 1 to 10 tons per hour. This ensures that the mechanical parameters align perfectly with the biochemical realities of the fruit.
The loss of that signature ruby-red hue in pomegranate juice is primarily a symptom of oxidation, excessive heat, and improper handling of delicate anthocyanins. Natural formulation adjustments provide a helpful layer of protection against these elements. However, the ultimate solution lies in the mechanical integrity and fluid dynamics of your processing hardware. You can identify the critical weak points causing degradation by auditing your current extraction stations, separation centrifuges, and packaging lines. Upgrading to closed-loop, low-temperature processing technology is a necessary investment. It empowers your facility to consistently deliver the vibrant, premium beverage that today's discerning consumers demand.
If your facility is struggling with product discoloration or low extraction yields, it is time to evaluate your processing infrastructure. For tailored engineering solutions, specialized extraction machinery, and complete custom production lines built to strict food-grade standards, explore the advanced equipment options available at WFoodMachinery to protect your product's quality and your brand's reputation.
It turns brown due to enzymatic browning and oxidation. Naturally occurring enzymes mix with oxygen in the air when the fruit is crushed. This rapid chemical reaction causes the natural red pigments to break down and degrade into brown compounds.
Gentle pressing extracts the liquid slowly without generating mechanical friction. Friction creates heat, and heat destroys the delicate pigments in pomegranates. This method naturally preserves the bright red appearance by keeping the temperature low and minimizing aeration.
Natural antioxidants do not significantly alter the flavor profile when used in the correct, precise dosages within an industrial setting. They may slightly enhance the natural tartness of the beverage while acting as a powerful, invisible shield against oxidation.
Aseptic or vacuum sealing environments are the most effective methods. These advanced technologies remove ambient oxygen from the bottle before the cap is applied. This prevents the liquid from oxidizing and losing its vibrancy while sitting in storage or on store shelves.
Yes, a centrifuge is necessary if your target market demands a clear, sediment-free product. A sanitary centrifuge efficiently spins out pulp and seed fragments in a completely closed environment. This clarifies the liquid quickly without exposing it to excess air, which is vital for maintaining quality before pasteurization.
Anthocyanins are highly sensitive to acidity levels. A lower, more acidic pH helps maintain the bright, stable red color. If the pH level rises and becomes more alkaline during processing or formulation, the pigments will structurally shift, turning the juice an unappealing blue, purple, or gray.
Yes, pasteurization can be achieved without destroying the color by utilizing High-Temperature Short-Time methods. By heating the juice to a high temperature for only 15 to 30 seconds and cooling it immediately, the machinery eliminates pathogens while minimizing the thermal residence time that typically cooks the red pigments.