Views: 0 Author: Site Editor Publish Time: 2026-10-01 Origin: Site


In the highly competitive dairy industry, profit margins are brutally tight. Waste management is no longer just an environmental checkbox; it is one of the most substantial daily operational expenses on the ledger. Every gallon of milk lost or byproduct wasted eats directly into a plant's bottom line. Traditional cheese manufacturing is inherently inefficient regarding material retention. Facilities frequently lose valuable whey proteins and generate massive amounts of sweet or acid whey. This creates a problematic liquid waste stream that costs a fortune to treat and dispose of properly.
To stop this financial bleed, modern dairy plants are revolutionizing how they handle raw materials before the coagulation process even begins. By leveraging advanced separation technologies, engineers can fundamentally alter the biochemical makeup of the starting liquids. This comprehensive guide explores exactly how upgrading your facility can eliminate waste, drastically boost production, and deliver a rock-solid return on investment for industrial dairy manufacturers.
Maximized Material Utilization: Upgrading to modern filtration systems allows dairy processors to retain up to 20% more whey proteins typically lost in traditional manufacturing. This directly converts raw material waste into sellable consumer products.
Significant Volume Reduction: By concentrating milk before the coagulation phase, plants process significantly smaller overall liquid volumes. This conserves vat space and drastically reduces heating and cooling energy requirements.
Reduced Wastewater Costs: Advanced separation techniques divide raw milk into retentate for cheese and permeate containing water and lactose. This prevents raw whey from entering the drain, drastically lowering the biological oxygen demand in plant wastewater and avoiding municipal fines.
Consistent Quality Control: Precise standardization ensures uniform batch composition regardless of seasonal milk variations. This significantly lowers the risk of product rejection and subsequent material waste.
High Return on Investment: The simultaneous reduction in waste disposal costs and the increase in product yields make upgrading to a membrane-based processing system a highly profitable, data-backed investment.
To understand how waste is systematically eliminated, we must first define the underlying technology. A UF cheese processing line is an automated, industrial-scale dairy production system. It integrates advanced membrane technology to pre-concentrate milk prior to the addition of rennet and bacterial cultures. Unlike traditional methods where raw milk is poured directly into an open vat, this system fundamentally alters the milk's composition at the molecular level.
Picture the modern factory floor. Rather than sitting in massive holding tanks for hours, pasteurized milk is routed through a network of sanitary stainless-steel pipes into a filtration module. The operational mechanism relies on cross-flow dynamics. The system pumps the liquid under high pressure—typically between 4 to 10 bar—across the surface of a semi-permeable barrier. If you were to push the liquid directly through a filter, it would quickly lead to severe clogging. Instead, the fluid flows parallel to the surface.
This physical action separates the milk into two distinct streams. The membrane is engineered to trap larger molecules, specifically butterfat, casein, and crucial whey proteins. This forms a concentrated mixture known as the retentate. This optimized liquid serves as the perfect base for cheese making. Meanwhile, water, lactose, and soluble minerals pass through the microscopic pores to form a clear liquid known as the permeate. In the commercial dairy sector, this methodology has become the gold standard for producing soft and semi-hard varieties such as feta, cream cheese, camembert, and mozzarella. It gives manufacturers absolute control over moisture content and protein levels.
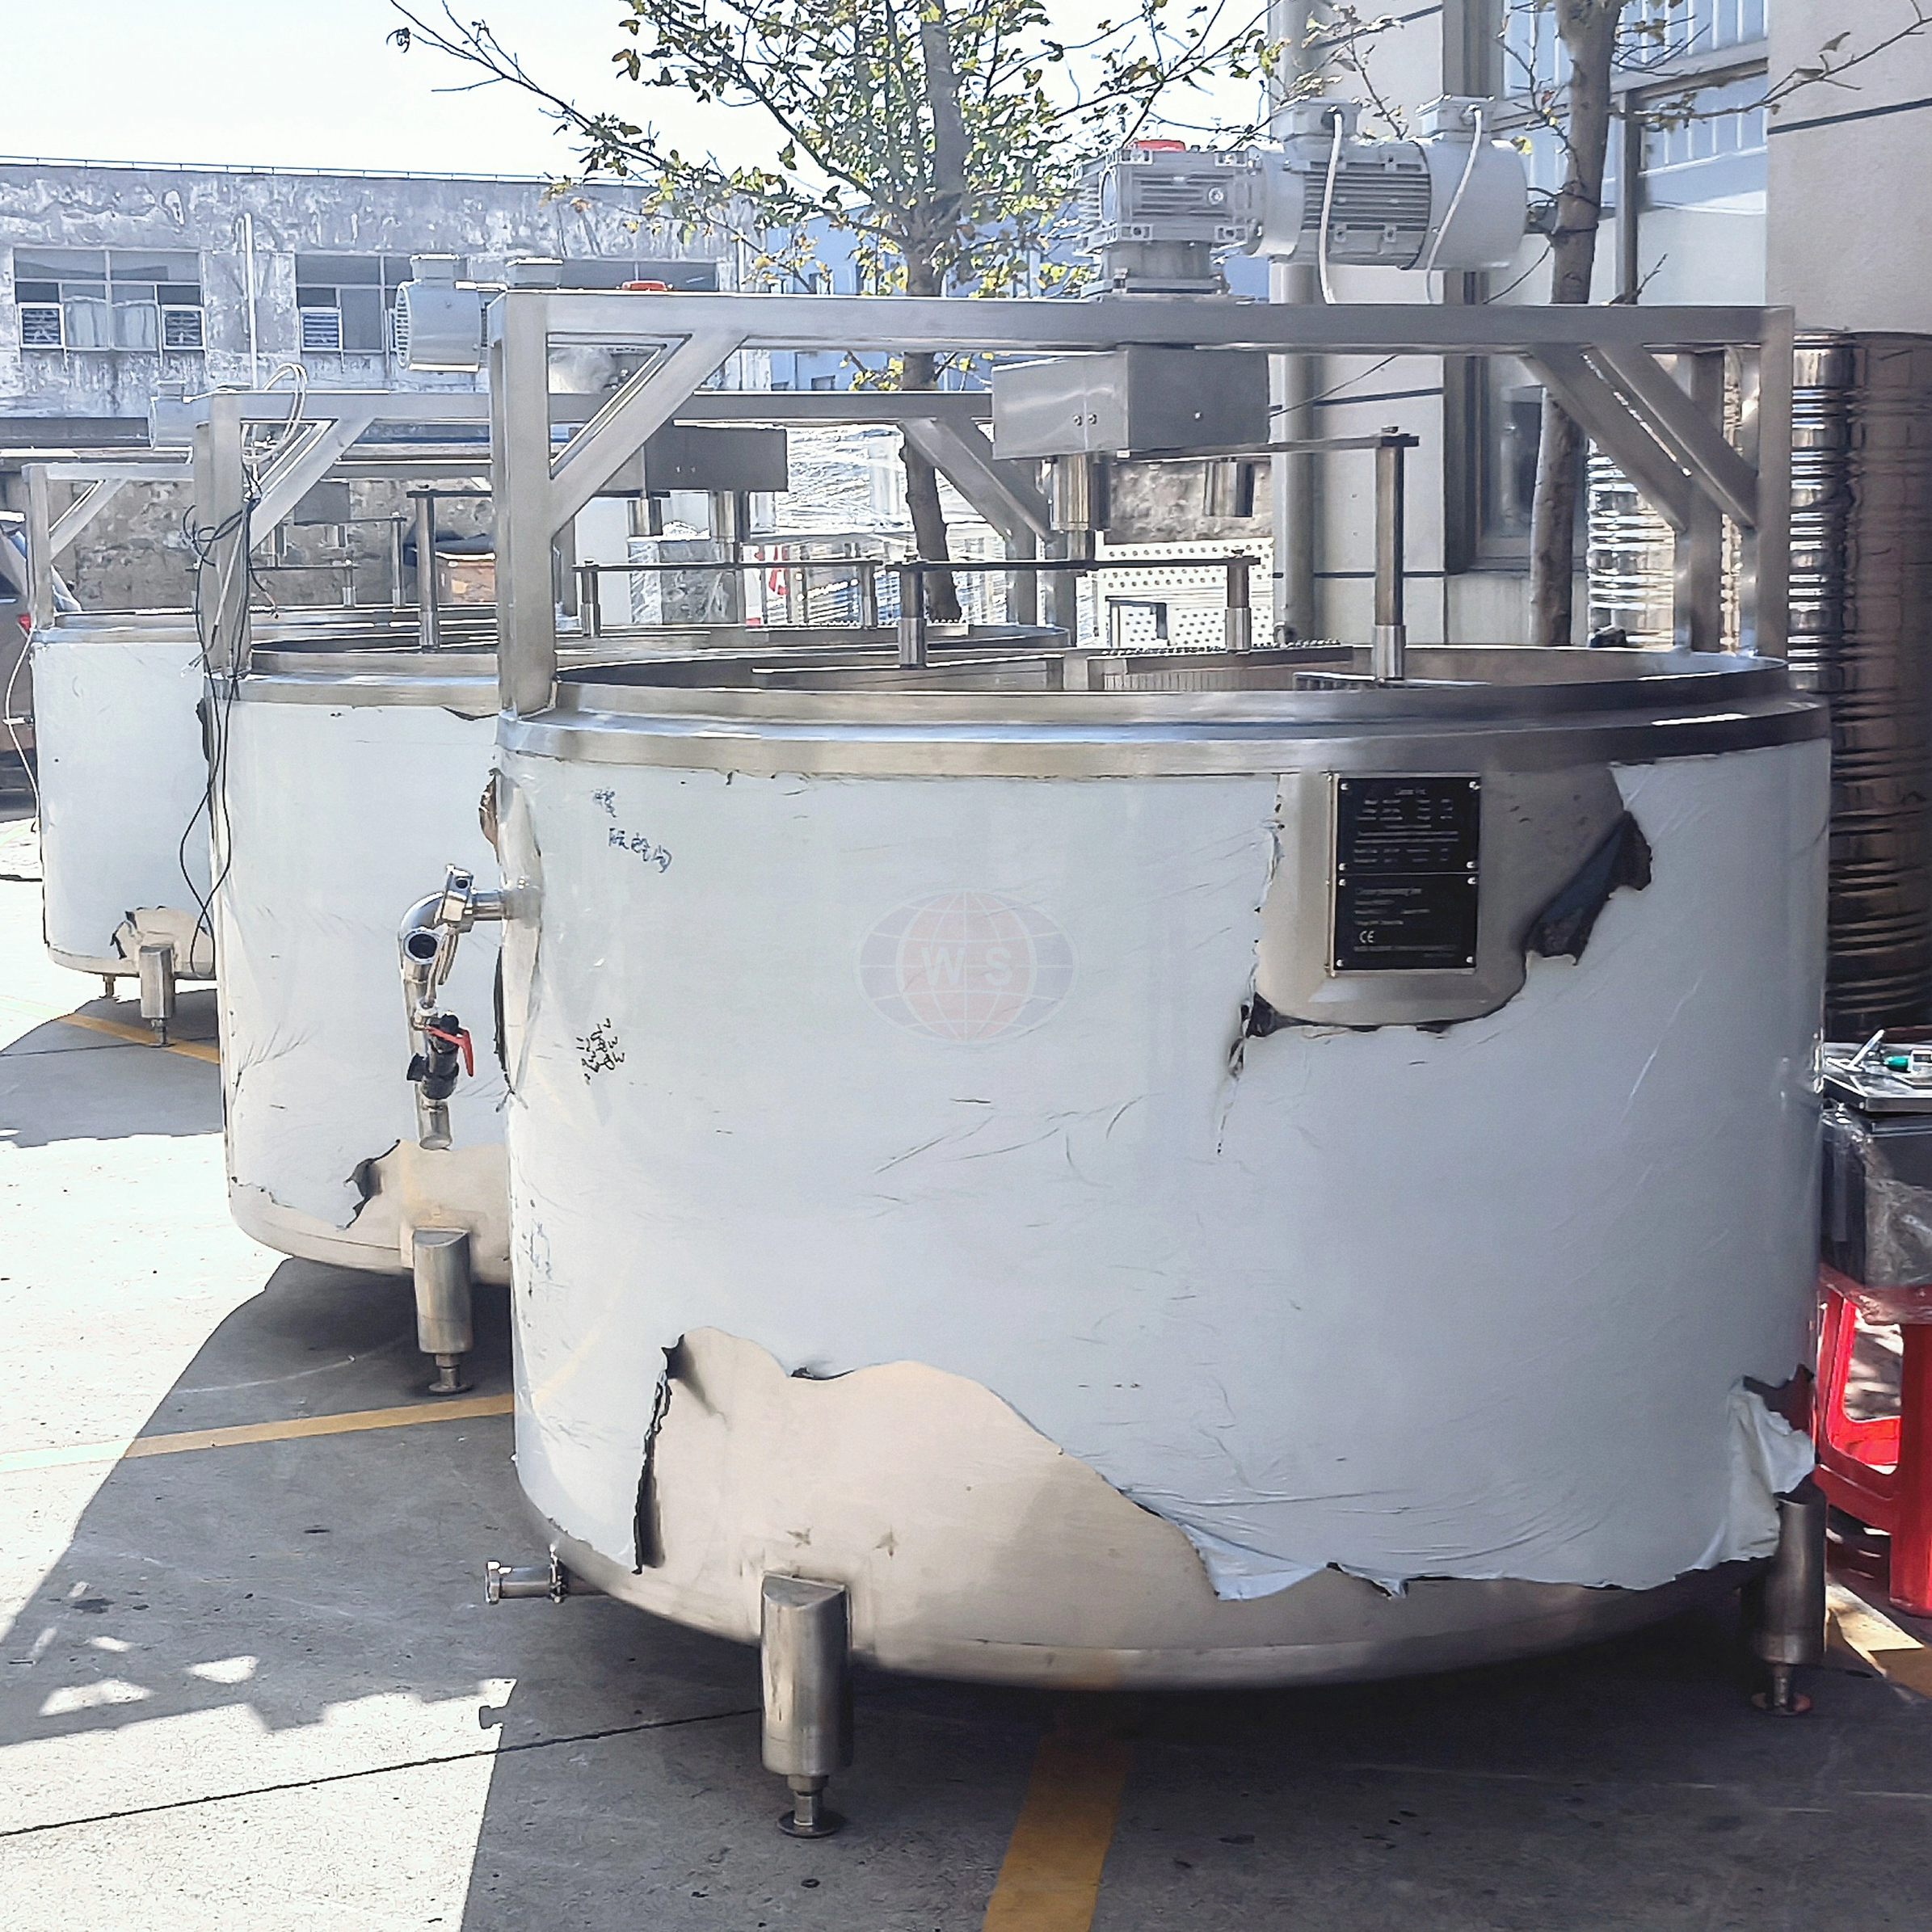
When evaluated through the lens of material retention, traditional cheese manufacturing is an inherently inefficient process. For centuries, the basic formula has remained unchanged: curdle the milk and drain the liquid. However, this rudimentary method produces approximately nine pounds of liquid whey for every single pound of cheese manufactured. For a medium-sized commercial dairy processing 100,000 liters of milk a day, this results in massive volumes of byproduct that must be managed immediately.
Looking at recent global dairy manufacturing trends, there is a massive regulatory push toward zero liquid discharge and circular economy models. Market analysts observe a distinct shift away from linear take-make-dispose manufacturing. Municipalities worldwide are severely tightening wastewater discharge limits. Facilities that treat whey merely as a disposable byproduct are facing crippling surcharges. Consequently, advanced ultrafiltration is transitioning from a niche technological upgrade to an essential baseline standard for regulatory compliance and economic survival in the modern era.
The first major loss in conventional setups is nutritional and financial. Traditional sweet or acid whey contains about 50% of the original milk's total solids, including highly valuable whey proteins. Unless a plant has invested millions of dollars in a separate, dedicated whey drying facility, these proteins are flushed out of the cheese matrix. This represents a severe loss of potential revenue. Furthermore, raw dairy whey is an environmental hazard. It possesses an exceptionally high Biological Oxygen Demand, often ranging between 35,000 and 50,000 mg/L. If discharged directly into municipal sewer systems, it rapidly depletes oxygen levels, prompting municipalities to impose severe financial penalties.
Implementing modern filtration fundamentally shifts a dairy plant from a high-waste operation to a highly efficient, closed-loop system. Specifically, there are five mechanisms through which this technology eliminates waste on the factory floor.
In conventional cheese making, whey proteins remain soluble in water and are drained away when the curds are cut. The integration of membrane filtration changes this physical dynamic entirely. The system captures soluble whey proteins like alpha-lactalbumin and beta-lactoglobulin, forcing them to remain alongside the casein and fat. When rennet is subsequently added, these proteins become physically trapped within the three-dimensional matrix of the curd. Empirical data shows this retention increases overall product output by 10% to 20% from the exact same starting volume of raw milk.
Because the milk is concentrated to the exact dry matter content required for the final product before coagulation begins, the traditional syneresis process is virtually eliminated. The retentate coagulates into a solid mass inside the packaging or the vat with little to no drainage required later. This liquid pre-cheese concept completely bypasses the generation of massive volumes of problematic liquid whey that traditional plants struggle to treat or transport.
The permeate extracted during the separation phase is a clean, predictable liquid consisting mostly of water, lactose, and minerals. Unlike raw whey, permeate is highly manageable. Modern facilities pipe this liquid directly into a Reverse Osmosis unit, which extracts pure water. This polished water is then recycled back into the plant's operations for Cleaning-In-Place systems or boiler feed water. This closed-loop approach slashes the plant's reliance on municipal water supplies and drastically reduces wastewater volume.
Raw milk is a natural product, meaning its composition fluctuates based on the season, the cows' diet, and lactation cycles. These fluctuations often lead to inconsistent moisture levels and textures, resulting in downgraded products or entirely rejected batches. Operators can now dial in the exact protein-to-fat ratio on their control screens, ensuring that every single batch meets strict quality control standards. Eliminating human error and natural variance prevents thousands of pounds of product from ending up in landfills.
Thermal energy waste is a hidden but massive expense in dairy processing. Heating raw milk to coagulation temperatures, maintaining that heat, and then cooling it requires immense amounts of steam and electricity. By concentrating the liquid first, the vats handle only a fraction of the original volume. Heating and pumping 2,000 liters of concentrated retentate requires exponentially less energy than processing 10,000 liters of raw milk, cutting the plant's carbon footprint and utility waste.
The operational success of this waste-reduction strategy rests entirely on the engineering of the UF membrane. Acting as the physical barrier separating valuable product from water, this component must operate with extreme precision and durability in harsh industrial environments.
These barriers operate in a specific pore size range, typically between 1 and 100 nanometers. This microscopic sizing translates to a 10 to 50 kDa molecular weight cut-off, which is perfectly calibrated for the dairy industry. The pores are small enough to block proteins and fat globules but large enough to allow water molecules and dissolved lactose to flow through freely. This selective permeability is what allows the system to extract waste water without losing a single gram of valuable protein.
In addition, modern materials contribute significantly to the sustainability of the plant. Historically, early filtration systems suffered from rapid fouling, requiring harsh chemical cleaners and frequent replacements. Today, facilities utilize advanced spiral-wound polymeric or robust ceramic variants. Ceramic models are highly resistant to extreme pH levels and high temperatures. They can withstand rigorous, automated cleaning protocols without degrading, often lasting up to ten years. This minimizes the physical waste generated by the processing line itself.
To fully grasp the waste-reduction capabilities of these systems, it helps to look at a standardized, data-driven comparison. When processing 10,000 liters of standardized raw milk into a soft cheese, the material flow differs drastically between conventional methods and modern filtration.
| Metric per 10,000L Raw Milk | Traditional Method | Ultrafiltration Method |
|---|---|---|
| Total Yield | Approx. 1,200 kg | 1,400 to 1,450 kg |
| Whey Protein Loss | ~60 kg flushed away | Near 0 kg - Fully retained |
| Byproduct Generated | 8,500L High-BOD Raw Whey | 8,000L Clean, Recyclable Permeate |
| Rennet Consumption | 100% Baseline | Reduced by up to 80% |
In a traditional setup, the baseline material input generates approximately 8,500 liters of raw whey, flushing out roughly 60 kilograms of valuable whey proteins. In contrast, the modern method retains nearly 100% of those whey proteins. Instead of high-BOD waste, it produces about 8,000 liters of clean, recyclable permeate. Furthermore, because enzymes are dosed for the concentrated retentate, up to 80% less rennet is wasted.
Ultimately, this technological shift translates directly to a cheese yield increase of 15% to 20%. More product per drop of milk inherently means less wasted raw material and a significantly higher revenue ceiling for the manufacturer.
For dairy plant managers and financial stakeholders, the decision to overhaul existing infrastructure hinges on empirical data and a verifiable return on investment. Integrating advanced technology requires a substantial initial capital expenditure. However, when evaluating the long-term operational economics, the transition from traditional vat coagulation to membrane-assisted processing presents a highly compelling financial case.
The core financial benefit lies in the drastic reduction of waste management expenses coupled with a simultaneous increase in marketable product. Operational savings begin to accrue from the very first production run. The payback period varies depending on plant capacity and local utility costs, but empirical industry data suggests that most medium-to-large facilities recover their investment within 18 to 36 months.
Several key factors accelerate this return. First, the immediate increase in production volume means more packaged goods to sell without purchasing additional raw materials. Second, mitigating wastewater surcharges provides immediate relief to the monthly operating budget. Plants situated in municipalities with strict environmental regulations often see their treatment costs plummet by over 60%. Finally, the reduction in thermal energy consumption and the lowered reliance on expensive coagulants ensure leaner utility and procurement bills.
Transitioning to membrane-based dairy processing is not a one-size-fits-all endeavor. Selecting the appropriate equipment requires a meticulous assessment of your facility's current production metrics, future growth projections, and the specific biochemical requirements of your product portfolio.
The first step is accurately matching the throughput of the unit to your plant’s intake capacity. Commercial systems typically range from 500 L/H for boutique operations up to 10,000 L/H or more for industrial scales. It is critical to calculate your desired Volume Concentration Factor. For example, fresh cheeses may require a concentration factor of 2x to 3x, while other applications might demand up to 5x. Precise milk concentration prevents production bottlenecks.
Additionally, prioritize material quality and automation. Ensure the equipment utilizes sanitary stainless steel, such as SUS304 or 316L, for all contact parts to maintain strict hygiene standards. Modern dairy processing relies heavily on robust control systems. Demand Siemens or Allen-Bradley logic controllers paired with inline sensors that continuously monitor Brix levels, protein-to-fat ratios, and flow rates. Partnering with specialized dairy machinery experts guarantees that flow dynamics modeling and membrane selection are tailored precisely to your factory footprint.
A modern filtration and processing line is not just a tool for making cheese; it is a comprehensive waste-reduction and profit-maximizing system. By leveraging advanced separation technology to optimize liquid concentrations, dairy processors can eliminate the headache of whey disposal, conserve municipal water, and significantly boost their overall production yields.
In an era where sustainability and profitability must go hand-in-hand, clinging to traditional, high-waste methods places manufacturers at a severe competitive disadvantage. The data clearly demonstrates that minimizing byproduct generation directly correlates with lower operational costs and higher revenue. Do not let valuable proteins wash down the drain. If you are ready to upgrade your facility, explore the high-performance, customizable commercial systems available at WFoodMachinery. Their engineering team can help you select the exact specifications needed to turn your waste stream into a profit center.
While highly versatile, this technology is most empirically proven and financially beneficial for fresh, soft, and semi-hard cheeses. Varieties such as Feta, Camembert, Cream Cheese, Ricotta, and Mozzarella benefit immensely from the retained whey proteins, which enhance their creamy texture. Hard cheeses, such as Cheddar or Parmesan, can also be manufactured using this concentrated milk. However, the process parameters must be carefully adjusted to ensure the curd achieves its required low moisture content and structural integrity during the aging stages.
From an organoleptic perspective, the process does not negatively alter the fundamental flavor profile. Because valuable whey proteins are retained alongside casein and fat, the resulting texture is frequently described as slightly smoother and creamier. Blind taste tests indicate that the vast majority of consumers cannot detect a difference in taste compared to traditionally made products. In fact, many culinary professionals actually prefer the enhanced mouthfeel and superior nutritional profile that this method provides.
The lifespan depends heavily on the material composition, operating pressures, and adherence to strict Cleaning-In-Place protocols. Spiral-wound polymeric models, which are standard in many facilities due to their cost-effectiveness, typically have an operational lifespan of 12 to 18 months before flux rates begin to decline. Conversely, ceramic models represent a higher initial investment but offer exceptional durability. They often operate efficiently for up to 10 years or more, significantly minimizing equipment waste.
The permeate generated is a clear liquid consisting primarily of water, lactose, and soluble milk minerals. In a waste-conscious dairy plant, this byproduct is never discarded. Instead, it is typically routed through a Reverse Osmosis system to extract pure, potable water. This water can then be safely reused within the facility for cleaning or boiler feed. The remaining concentrated lactose can be dried into powder and sold globally as a high-value ingredient for infant formula or agricultural animal feed.
Yes, empirical data confirms a significant reduction in additive consumption. Because precise concentration occurs prior to the coagulation phase, operators introduce coagulants, rennet, and expensive starter cultures to a much smaller volume of liquid rather than the entire volume of raw milk. The enzymatic kinetics in this concentrated state are highly efficient, routinely allowing plants to cut their consumption of expensive enzymes and cultures by 30% to 50%.
Ultrafiltration is designed to separate larger macromolecules. It retains proteins and fats while allowing water and lactose to pass through. Reverse Osmosis, on the other hand, operates with much tighter membrane pores. It is typically used downstream from the UF process to treat the permeate. RO blocks almost all dissolved solids, including lactose and minerals, allowing only pure water to pass through. Together, they create a complete liquid recovery system.
The ideal capacity depends directly on your daily raw milk intake and production goals. Entry-level commercial skids often process around 500 liters per hour, making them suitable for artisanal or regional dairies. Large-scale industrial plants typically deploy modular systems capable of handling 5,000 to 10,000 liters per hour. The modular nature of these systems allows facility managers to add extra membrane housings as production demand scales up over time.